

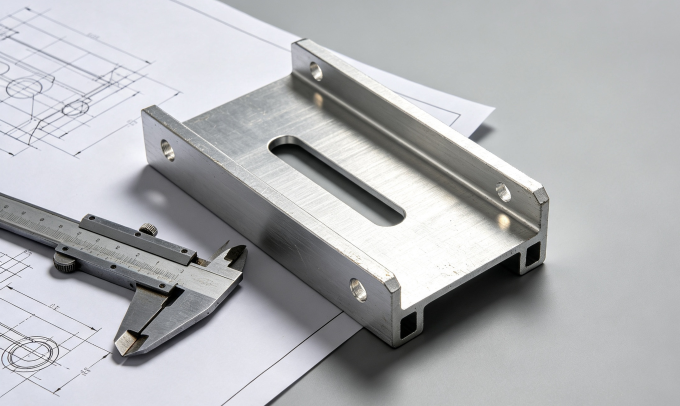
1. Geometric Features: Make Room for the Cutting Tool
CNC machining is fundamentally a process of relative motion between rotating cutters and the workpiece. Therefore, part geometry must respect the physical limits of those tools.
Always add radii to internal vertical corners. A sharp internal corner cannot be cleaned out by a standard end mill, because the tool itself has a radius. If a sharp corner is absolutely required, it will have to be achieved by EDM or manual finishing—both of which add significant time and cost. A simple best practice is to add a radius of at least 1 mm (or one‑third of the tool diameter) to every internal corner. This not only permits the use of larger, more rigid tools but also improves stress distribution and enhances part strength.
Avoid deep, narrow cavities. When cavity depth exceeds four times its width (for steels) or six times (for aluminium), long slender tools are prone to chatter and breakage. If such a feature is unavoidable, consider splitting the part into simpler components or using an alternative process like wire EDM. Also, for blind holes, always use a standard drill point angle (118° or 135°) rather than a flat bottom, unless the function explicitly demands it—flat‑bottom drills are non‑standard and prone to failure.
Design thin walls with care. Thin walls deflect and vibrate under cutting forces. For aluminium, keep wall thickness above 0.8 mm; for steel, above 1.5 mm. For plastics, increase these values further to prevent melting or warping from cutting heat. If thin walls are necessary, consider adding ribs or adjusting the machining sequence (rough first, then finish).
2. Tolerances and Threads: Don’t Over‑Specify the Small Stuff
Tolerances are the single biggest driver of machining cost. Every tightening of a tolerance adds extra inspection time, more frequent tool compensation, and a higher scrap rate.
Apply tight tolerances only where truly needed. Only critical mating surfaces require ±0.005 mm or tighter. All other dimensions should use the machine’s general capability, typically ±0.1 mm or ±0.05 mm depending on the material. Designers often habitually apply high tolerances across the entire drawing—this is one of the largest sources of wasted cost.
Standardise holes and threads. Whenever possible, design holes to match standard drill sizes; non‑standard diameters require custom tooling, increasing both cost and lead time. For threads, stick to standard coarse or fine series, and keep thread depth no more than 3× the nominal diameter—deeper threads demand special taps and raise the risk of breakage. For larger diameters or difficult‑to‑machine materials, specify thread milling instead of tapping; it is safer and more flexible.