

CNC MACHINED AL6061 BILLET RACK CLAMP
From concept to production in 25 days High-quality, cost-efficient rapid tooling solution.
25 Days
Total Lead Time
±0.02 mm
Precision Tolerance
100K+ Shots
Mold Life
0 PPM
Quality Target
Project Overview
This project involved CNC machining an Al6061 billet rack clamp for an off-road / custom vehicle application. The component is a split clamp-style structural mount with a Ø62 mm central bore, two mounting feet, threaded fastening features and sculpted external surfaces.
The production drawing identifies the part as BILLET RACK CLAMP, material Al6061, weight approximately 0.78 kg, with ISO 2768-fK applied to unspecified tolerances and an overall Ra 3.2 surface-finish requirement. The combination of a large clamp bore, split line, mounting features and cosmetic exterior surfaces meant that dimensional control and visible finish quality were both important.
Part | Billet Rack Clamp | Material | Al6061 |
Weight | Approx. 0.78 kg | Application | Off-road / custom vehicle |
General tolerance | ISO 2768-fK | Drawing finish | Ra 3.2 |
Key geometry | Ø62 clamp bore | Process | Multi-face CNC milling + finishing |
The Challenge
The first machining attempts were functionally workable, but the visible surfaces did not meet the appearance we wanted. The earlier production photo shows more obvious cutter marks and a comparatively dull, inconsistent finish on the broad sculpted surfaces.
This became an important manufacturing lesson: on an exposed billet component, surface quality depends not only on the drawing roughness requirement but also on tool geometry and sharpness, spindle speed, feed per tooth, radial/axial engagement, step-over, toolpath direction, runout and workholding rigidity.
Feed rate does matter, but it should not be treated as an isolated number. Excessive feed per tooth can make feed marks more pronounced, while an unnecessarily low feed can encourage rubbing rather than clean cutting. The finishing parameters must be matched to the tool and setup.
Tight Tolerance
Critical dimensions required ±0.02 mm tolerance.
Short Lead Time
Tooling and samples requested within 4 weeks.
High Cosmetic Requirement
No flow marks, no weld lines, high gloss surface.
Our Solution
Based on the early result, we revised the finishing process instead of relying on polishing to hide machining marks.
For the final finishing passes, we used a diamond cutting tool / diamond-edge finishing tool suitable for aluminum. Its very sharp cutting edge helped reduce built-up edge and produced a cleaner cut on the Al6061 surfaces. Roughing and finishing were separated, leaving controlled stock for the final passes.
We also optimized finishing feed, spindle speed, engagement and toolpath to reduce visible cutter transitions across the large cosmetic faces. Particular attention was given to the Ø62 clamp bore, split-clamp interface, mounting features and broad exterior surfaces. The improved production photos show clearer reflections, more uniform surfaces and noticeably reduced visible tool marking compared with the earlier trial.
DFM Analysis
1–2 Days
Rapid Tool Design
3–5 Days
CNC Machining
7–10 Days
Assembly & Testing
3–5 Days
Sample Approval
25 Days
Project Results
The final parts achieved a substantially cleaner and more consistent machined appearance while retaining the required functional geometry.
More importantly, this project created reusable process knowledge for future aluminum billet parts. When a customer expects a bright machined appearance, tool selection, feed per tooth, spindle speed, step-over, finishing allowance, runout and workholding must be treated as one finishing system.
This is valuable EEAT evidence because the improvement is supported by a real production drawing and actual before-and-after manufacturing photographs rather than a generic claim of “high-quality machining.”
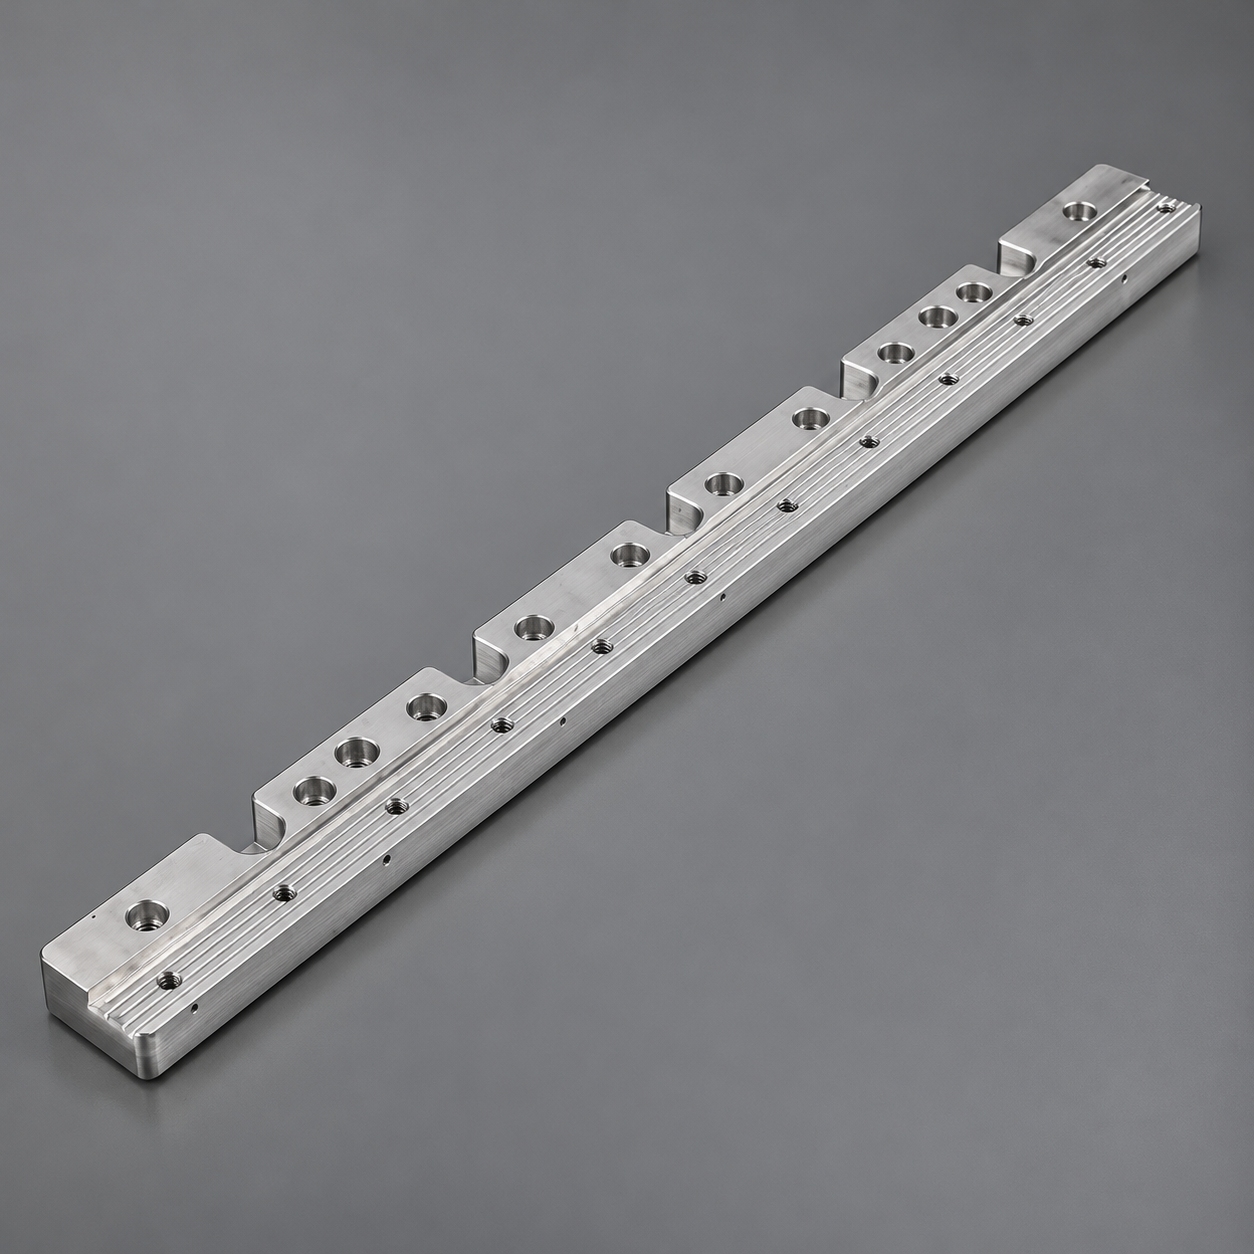
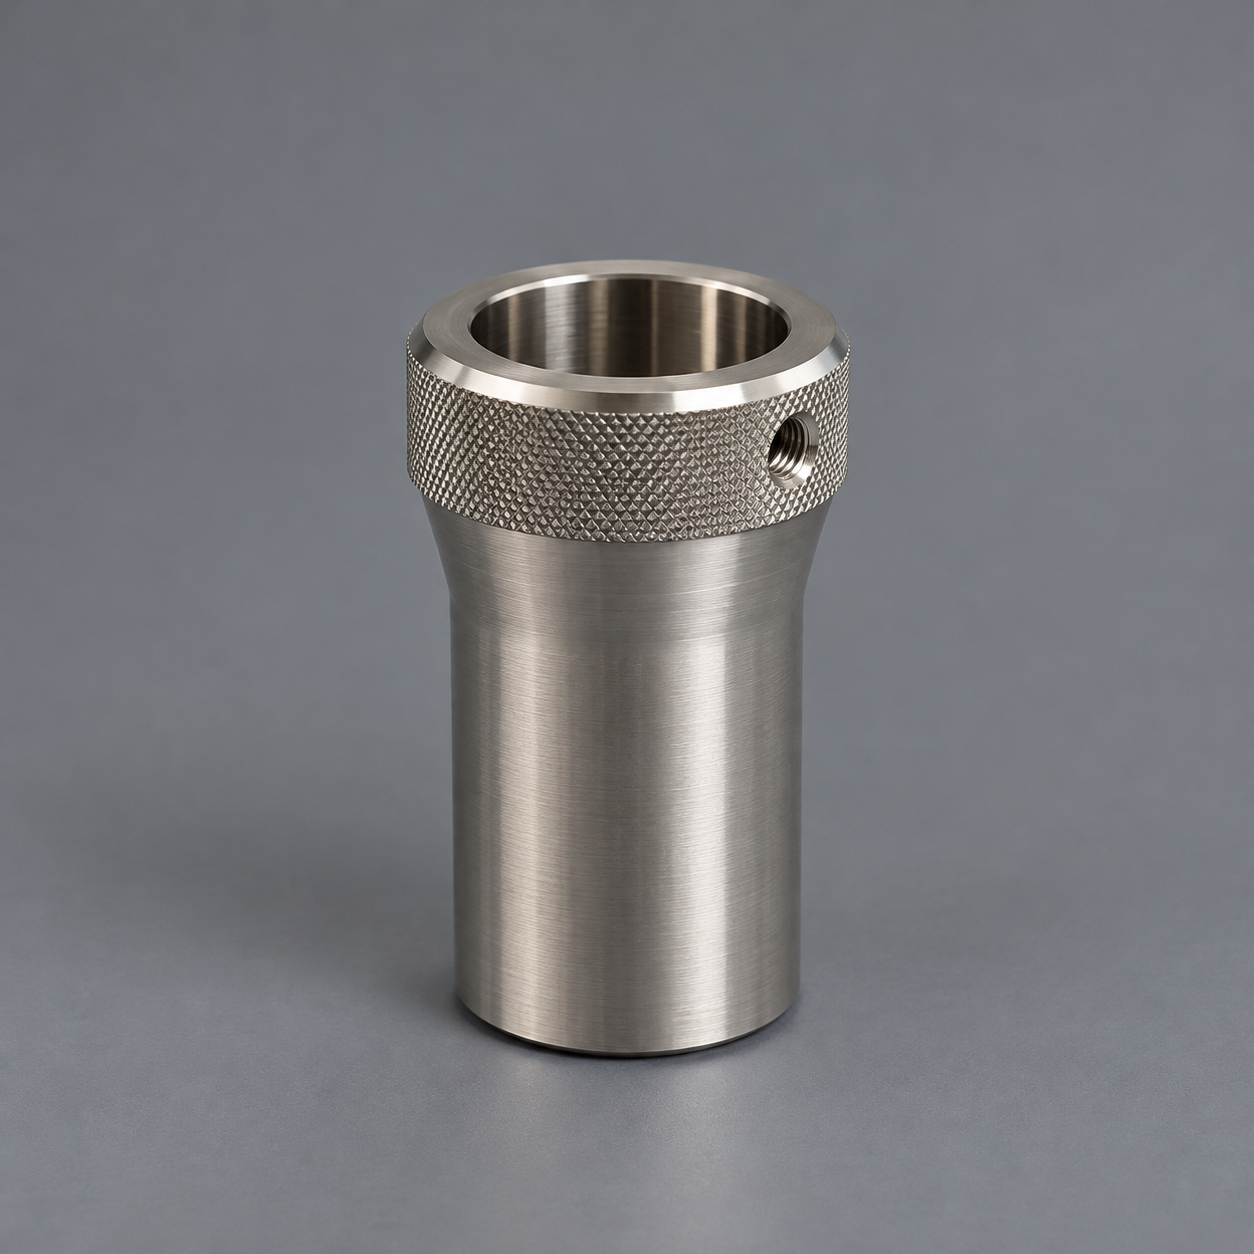
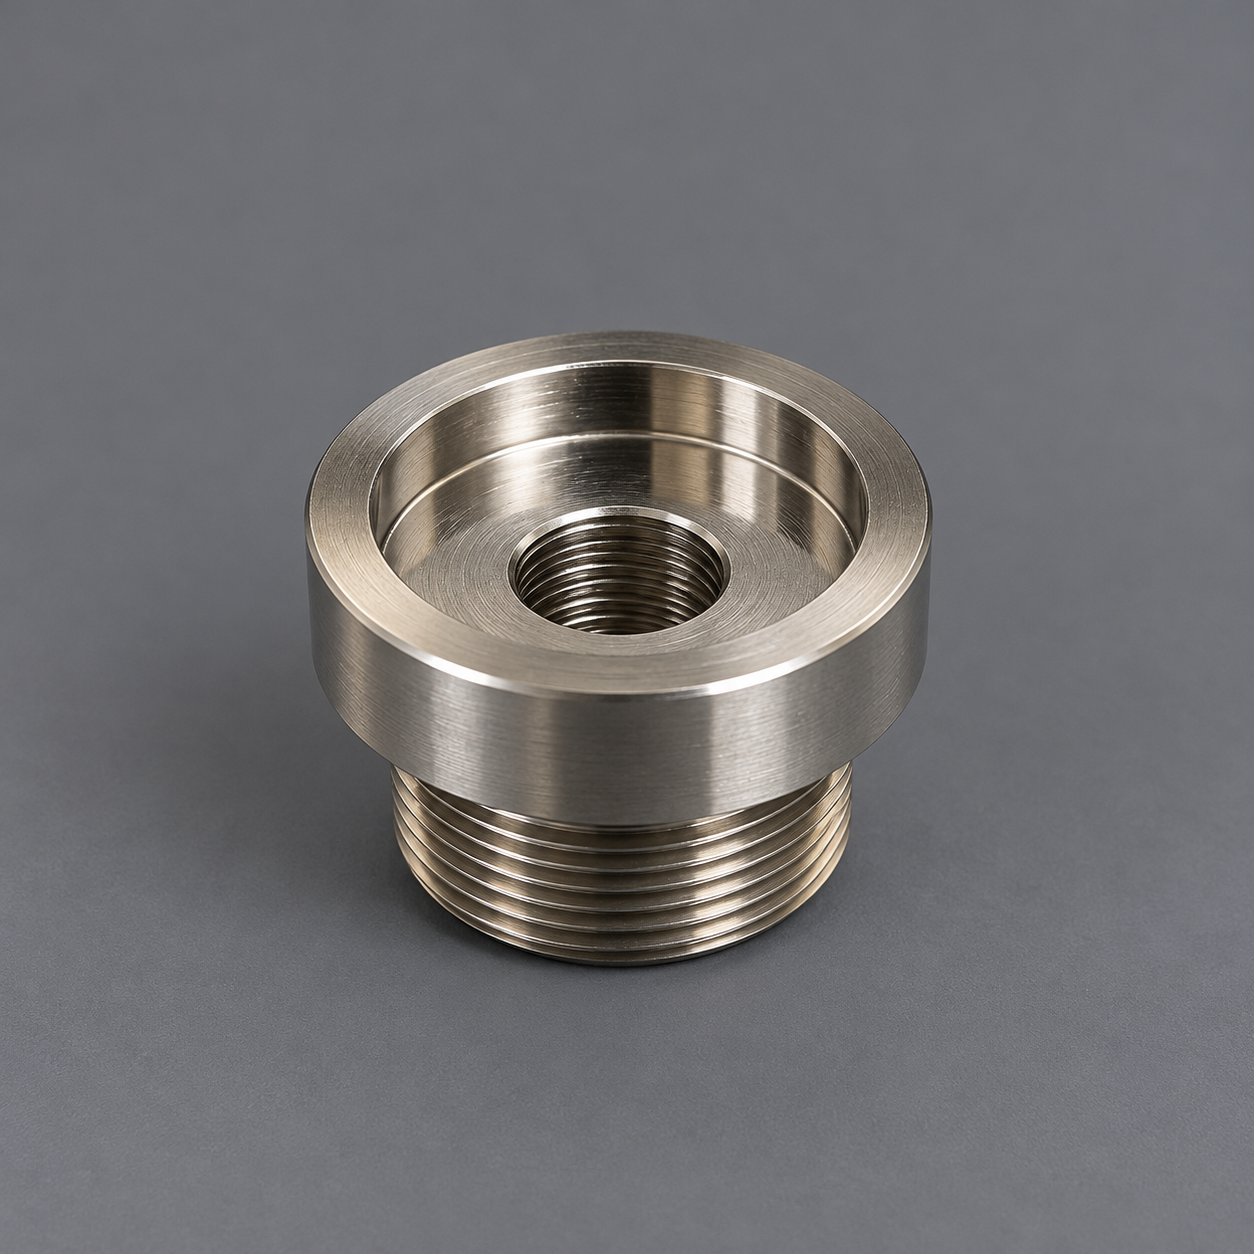
Project Photos

Customer Feedback
“
The tooling quality exceeded our expectations. The parts met all requirements and the lead time was impressive. We highly recommend their rapid tooling service.
— Project Manager, Automotive Lighting Company
Why Choose Us
10+ Years
Industry Experience
1000+
Successful Projects
Advanced Equipment
Precision Manufacturing
Strict Quality Control
ISO 9001 Certified
Global Service
Local Support